High-Precision Assembly Line AGVs & Autonomous Forklifts
Engineered for continuous 24/7 material flow, tight-aisle line-side docking, and direct carrier interlock across modern discrete manufacturing workcells.
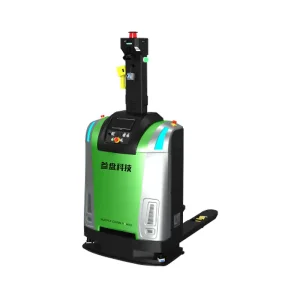
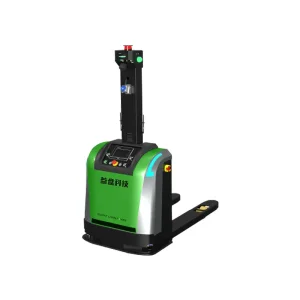
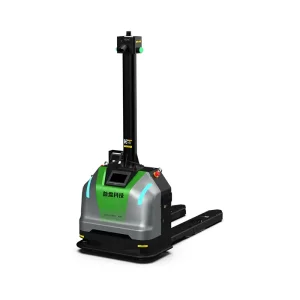

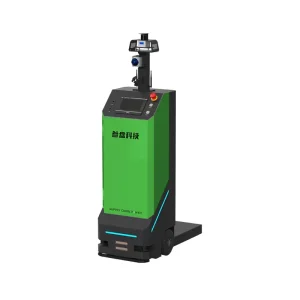
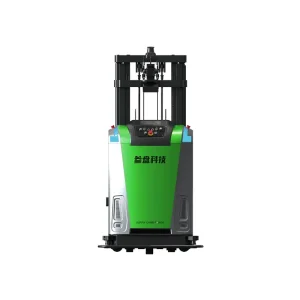
The Industrial Evolution of Assembly Line AGVs & Autonomous Logistics
In modern industrial manufacturing, the transition from fixed conveying infrastructure—such as rigid roller tracks, continuous drag chains, and overhead monorails—to agile Autonomous Guided Vehicles (AGVs) and Autonomous Mobile Robots (AMRs) represents the most critical operational paradigm shift of Industry 4.0. Contemporary production lines in automotive, high-rate electronics, consumer durables, and clean energy battery fabrication demand unprecedented operational flexibility, dynamic balancing, and just-in-sequence (JIS) part feeding.
Historically, traditional assembly plants relied on buried magnetic wire or optical reflective targets to guide automated haulers. While effective in stable settings, these legacy systems incur prohibitive downtime and infrastructure modification costs whenever takt schedules change, workstations expand, or production cell layouts are altered. Today's Tier-1 industrial AGVs utilize advanced Laser SLAM (Simultaneous Localization and Mapping) combined with 3D multi-spectral perception and edge-computed trajectory planning. This enables true reflector-free natural navigation that maps up to 400,000 m² in a single coordinate coordinate frame while executing sub-centimeter line-side docking alongside human workcells.
Zero-Infrastructure Deployment
Laser SLAM eliminates magnetic strips, floor cutouts, and retroreflective wall prisms. Rapid mapping protocols allow complete shopfloor coordinate calibration within 24 to 48 hours without halting ongoing assembly shifts.
Dynamic Workcell Balancing
Unlike rigid continuous conveyor belts, assembly AGVs turn static assembly lines into dynamic, matrix-style work hubs. If a bespoke vehicle build requires higher labor duration at Station 4, the fleet dispatcher dynamically redirects downstream units to clear bottlenecks.
Deterministic Line-Side Safety
Equipped with dual safety-rated safety LiDAR scanners (SIL2, PLd certified) and 3D visual cameras, modern assembly AGVs detect low-lying forks, overhead projections, and erratic foot traffic, ensuring uninterrupted collision-free collaborative operation.
Why Tier-1 Plants Choose Chinese Assembly Line AGV Manufacturers
The global shift toward Chinese robotic intralogistics is driven by comprehensive supply chain integration, superior iteration velocity, and unmatched price-to-performance metrics.
Complete Component Cluster Density
China hosts the world's most concentrated ecosystem for mobile robotic sub-assemblies. From solid-state LiDARs and precision planetary gearboxes to heavy-duty steering drive assemblies and industrial grade lithium iron phosphate (LiFePO4) battery packs, raw procurement lead times are condensed from months to days.
Aggressive Engineering Iteration Cycles
Chinese assembly line AGV factories leverage rapid prototyping and concurrent design engineering. Customizing a bespoke carrier interface, automated scissor lift, or dual-roller motorized conveyor top takes an average of 3 to 5 weeks from initial CAD approval to physical factory floor testing.
Total Cost of Ownership (TCO) Dominance
Delivering high-performance hardware and modular fleet management software at 40% to 60% lower capital expense than Western legacy counterparts enables multi-national enterprises to compress their operational payback periods from typical 36-month cycles down to under 12 to 18 months.
Stress-Tested in World-Class Mega-Plants
Chinese AGVs have been refined through deployment in the world's largest automotive gigafactories, solar module assembly plants, and consumer electronics assembly lines. This harsh, high-throughput operating environment weeds out mechanical and software edge-case bugs before export.
Open Protocol & Multi-Vendor Interoperability
Leading Chinese builders adopt open architecture, fully supporting VDA 5050, MQTT, Modbus-TCP, and RESTful APIs. This prevents proprietary vendor lock-in, enabling overseas clients to blend AMR chassis with pre-existing warehouse management and manufacturing execution systems.
Emerging Technology Trends in Modern Assembly Line Robotics
Breakthrough innovations that distinguish cutting-edge intralogistics robots from outdated cart haulers.
1. Hybrid Multi-Sensor Fusion SLAM
Pure optical visual SLAM struggles in environments with dynamic overhead cranes or fluctuating natural illumination, while pure 2D LiDAR SLAM can be disoriented in long, uniform factory corridors with repeating structural beams. Next-generation assembly AGVs integrate hybrid localization: fusing multi-line 3D LiDAR point clouds, visual stereoscopic odometry, wheel IMU dead-reckoning, and ground texture recognition. If sudden changes obscure 70% of environmental features, the AGV maintains tracking continuity with sub-millimeter precision.
2. Edge-AI Vision for Automatic Carrier & Pallet Pose Estimation
In real-world assembly environments, human workers or forklifts do not drop bins, racks, or pallets with mathematical precision. Advanced assembly line AGVs now possess deep-learning edge vision running on onboard neural network processors. The AGV scans incoming staging stands, identifies skew, tilt, and pallet hole dimensional deviations in 3D, and computes real-time kinematic adjustments to insert forks or lift pins smoothly without wedging or spilling fragile components.
3. Opportunistic Ultra-Fast Charging & 2-Minute Swappable Power
To achieve uninterrupted 24/7 assembly continuity, current fleets utilize high-rate lithium-iron batteries capable of 2C to 3C charging. Automated ground contact charging plates allow AGVs to absorb quick charges during takt pauses at assembly stations (15 seconds to 2 minutes), sustaining continuous operations without returning to isolated charging bays. For mission-critical continuous cycle schedules, mechanical dual-battery swap designs allow battery exchange within 120 seconds.
| Technical Dimension | Legacy Magnetic / Reflector AGV | Modern Laser SLAM AMR / AGV |
|---|---|---|
| Deployment Footprint | Floor slots, magnetic adhesive tape, reflector pillars | Reflector-free natural feature mapping; 100% virtual routes |
| Line-Side Route Changeover | Requires 2-4 days of physical labor & downtime | Software drag-and-drop map adjustment in minutes |
| Obstacle Reaction | Static stop until obstacle is manually removed | Dynamic 3D clearance calculation & smooth auto-bypass |
| Docking Precision | ±10 mm to ±25 mm without mechanical guides | ±5 mm standard (±2 mm with secondary visual alignment) |
| Fleet Orchestration Scale | Limited to 10-30 units before route deadlocks occur | Scales to 500+ units under centralized VDA 5050 cloud RCS |
High-Impact Assembly Line Application Scenarios
How assembly line AGVs unlock throughput gains and eliminate manual bottlenecks across specific shopfloor settings.
Automotive Powertrain & Chassis Marriage
Dual-drive counterbalanced and lifting AGVs serve as mobile assembly platforms for engines, e-axles, and battery packs. Synchronized with overhead body conveyors, the AGV drives underneath the chassis, raising the complete powertrain into the vehicle body with millimeter-level geometric repeatability.
New Energy Lithium-Ion Cell Assembly
Operating inside cleanroom environments (ISO Class 6), customized AGVs carry heavy electrode rolls and cell modules. Featuring non-particulate polyurethane drive wheels, stainless steel covers, and ESD static dissipation protection, they prevent fire risks and maintain cleanroom standards.
3C Electronics & SMT Line-Side Kitting
In high-density electronics plants, compact AMRs slide underneath component roll carts, automatically delivering reels, PCB magazines, and soldering consumables to SMT lines. Tight body widths (under 750 mm) allow smooth operation in narrow 1.2-meter aisles without human interference.
Heavy Machinery & Large Wind Turbine Assembly
Handling components weighing 5 to 30 metric tons requires tandem-coordinated omnidirectional AGVs. Using virtual mechanical link protocols over ultra-reliable low-latency 5G/Wi-Fi 6 networks, two or more AGVs collaborate under master-slave logic to carry massive turbine housings safely through assembly stages.
End-to-End Shopfloor Software & Fleet Orchestration
An assembly line AGV is only as capable as the enterprise software coordinating its movements.
A standard mistake in shopfloor robotics procurement is evaluating the physical mobile vehicle in isolation from the digital dispatch ecosystem. Achieving a zero-starvation assembly line requires real-time orchestration across the manufacturing hierarchy:
Level 4: Enterprise ERP & MRP
Maintains macro bill of materials (BOM), production forecasting, supplier shipment status, and finished unit order books.
Level 3: MES & Line-Side WMS
Generates cycle-time pull triggers (electronic Kanban), monitoring workstation progress and issuing material calls when parts fall below safety thresholds.
Level 2: Robot Control System (RCS)
Calculates holistic traffic routings, resolves intersection locks, prioritizes high-urgency part calls, and balances opportunistic battery charging states.
Level 1: On-Board Motion Controller
Executes closed-loop kinematics, handles obstacle safety zones, and coordinates lifting mechanisms, motorized rollers, or clamps at the workcell interface.
Our solutions feature open APIs that connect natively with SAP, Oracle, Siemens Opcenter, and custom MES architectures via standard RESTful, MQTT, or OPC-UA protocols. By harmonizing warehouse buffer storage, kitting zones, and live assembly workstations, line starvation risks are reduced by over 99%.
Global Enterprise Procurement Matrix: How to Audit an AGV Factory
Essential criteria engineering directors, supply chain leaders, and procurement heads must evaluate before signing equipment contracts.
Functional Safety Compliance (ISO 3691-4)
Never compromise on safety certifications. Ensure the manufacturer validates the entire safety chain—sensors, emergency stops, safety PLCs, and drive cutoffs—in compliance with EN ISO 3691-4:2020 and ANSI/ITSDF B56.5 standards. Demand Performance Level d (PLd) certificates from recognized third-party test houses.
Mean Time Between Failures (MTBF)
Validate real-world reliability metrics. Tier-1 assembly line suppliers demonstrate audited MTBF figures exceeding 5,000 continuous hours. Scrutinize component selection: are they using industrial-grade servo drives, reputable Japanese or European harmonic reducers, and heavy-duty structural steel?
Global Lifecycle Support & SLA Terms
Examine the supplier's overseas support model. Do they offer guaranteed remote response windows (under 2 hours), local system integrator partnerships for physical intervention, and a transparent spare parts warranty? Verify that primary electronics are modular and field-replaceable within 30 minutes.
Frequently Asked Questions: Assembly Line AGV Integration
Authoritative answers to core engineering, deployment, and operational queries from enterprise manufacturing leaders.
How does Laser SLAM maintain positioning accuracy when factory environments change constantly?
What floor flatness and surface conditions are mandatory for reliable assembly AGV operation?
Can these assembly AGVs pass through automated fire doors and ride freight elevators between floors?
What standard communication protocols connect the fleet system to existing enterprise software?
What is the real-world operational lifespan of lithium battery systems under heavy three-shift production?
How long does physical on-site deployment and commissioning typically take?
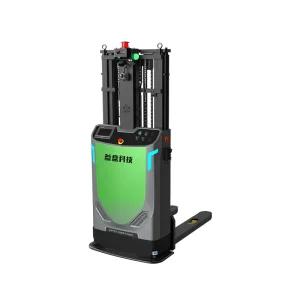
High-Payload Stackers, Mobile Chassis & Narrow-Aisle AGVs
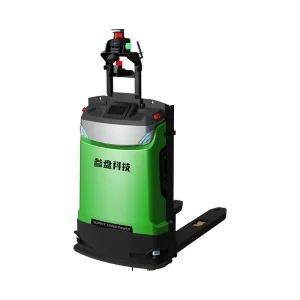
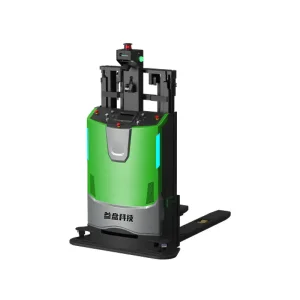
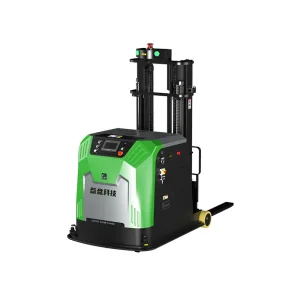
Heavy counterbalanced lifters, autonomous stacking robots, and agile mobile chassis tailored for demanding assembly operations.