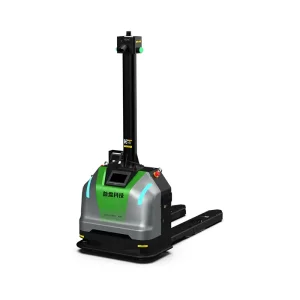
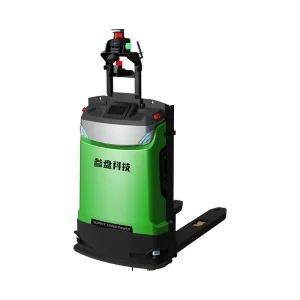
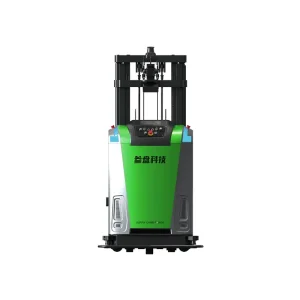
High-Precision Magnetic & Laser Navigation Autonomous Fleet
Engineered for high-throughput factory lines, narrow aisles, and continuous 24/7 mission-critical intralogistics. Explore our flagship models engineered with industrial-grade docking accuracy.

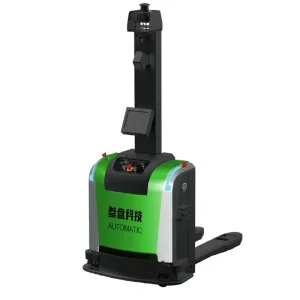
Engineering Superiority: The Enduring Dominance of Magnetic Tape Navigation
Why modern automated guided vehicles (AGVs) and intelligent material handling ecosystems continuously deploy magnetic tape guidance alongside hybrid optical modalities.
Deterministic Hall-Sensor Physics
Magnetic tape navigation leverages multi-channel Hall-effect sensor bars that sample magnetic flux density (typically between 100 and 1,000 Gauss) at sample rates exceeding 1,000 Hz. Unlike optical vision or ambient laser triangulation, magnetic tracking is mathematically deterministic, completely immune to airborne dust, ambient lighting flux, surface gloss changes, and industrial vapor clouds.
Sub-Millimeter Lateral Precision
By computing differential field strength across 16-bit array channels, the on-board industrial AGV controller achieves dynamic steering corrections with an operational tolerance of ±2 mm to ±5 mm. This mechanical precision is essential for docking into automated high-density rack storage, machine-tool indexing fixtures, and heavy robotic roll conveyors where misalignments yield catastrophic line stalls.
Immunity to Dynamic Feature Fluctuation
Laser SLAM relies heavily on static ambient architectural boundaries (walls, structural pillars). In high-turnover logistics distribution hubs where staging pallet heights shift hourly, pure SLAM maps experience feature degradation and localization drift. Magnetic strip navigation provides an absolute ground-truth coordinate trajectory that never 'loses tracking'.
Navigation Paradigm Benchmark: Magnetic vs. SLAM vs. QR Codes
An engineering benchmark comparing capital expenditure, deployment velocity, environmental resilience, and lifecycle operational cost (TCO).
| Navigation Modality | Docking Precision | Ambient Sensitivity (Dust/Steam) | Floor Retrofit Complexity | Route Modification Speed | 5-Year TCO Rating |
|---|---|---|---|---|---|
| Magnetic Tape (Ferrite / Neodymium) | ±2 mm to ±5 mm | Complete Immunity (100%) | Low (Surface Tape or 2mm Slit) | Immediate Physical Relay | Lowest Capex & Zero Licensing |
| Laser SLAM (Natural Feature) | ±5 mm to ±10 mm | High (Smoke/Dust Scatters LiDAR) | None (Virtual Mapping) | Software Re-mapping | Moderate to High (Costly Sensors) |
| Inertial QR Code Matrix | ±3 mm | Vulnerable (Scratches/Grease) | Moderate (Tile Placement Grid) | Grid Relocation | Moderate (Frequent Code Replacement) |
| Dual Hybrid (Magnetic + Laser SLAM) | ±1 mm to ±3 mm | Dynamic Redundancy Failover | Selective High-Precision Gates | Hybrid Software/Physical Layer | Optimal Balance for Mega-Factories |
China Factory Ecosystem: Unrivaled Supply Chain Integration
How Sichuan and China’s advanced robotics manufacturing clusters deliver 40%–60% capital advantages, rapid custom engineering, and mission-grade build quality.
Vertical Hardware Component Integration
By consolidating structural laser-cut chassis fabrication, high-torque brushless DC steering motors, integrated planetary gearboxes, and automated SMT board manufacturing within 100-kilometer localized supply clusters, our factory slashes component lead times from months to days while amortizing tooling overhead across massive production volumes.
Proprietary Controller & Firmware Stack
Rather than relying on closed third-party industrial black boxes, our factory manufactures proprietary SCC controllers and Server X Store fleet controllers. This in-house hardware IP grants overseas procurement directors comprehensive open-API hooks, seamless CAN-bus integration, and firmware-level adaptability without recurring per-seat software licensing fees.
Strict Quality Verification (FAT & SAT)
Every automated vehicle undergoes a mandatory 72-hour burn-in regimen, multi-axis laser kinematic alignment, dynamic payload deflection load tests (up to 3,000 kg capacity), and thermal chamber validation before export crating. Factory Acceptance Testing (FAT) documentation accompanies every unit, ensuring predictable on-site commissioning.
ISO 3691-4 Safety Compliance & Functional Certification
Ensuring cross-border compliance across North America, Europe, Australia, and Asia-Pacific industrial safety standards.
EN ISO 3691-4:2023 & ANSI B56.5
Modern driverless industrial trucks must comply with stringent functional safety mandates. Our AGVs incorporate Category 3, Performance Level d (PL-d) certified safety architecture, utilizing dual-channel monitored E-stop loops, certified safety PLCs, and fail-safe electromagnetic brake release mechanisms.
Dynamic Multi-Zone Safety Scanners
Equipped with dual 270° safety laser scanners operating seamlessly alongside magnetic floor trackers, vehicles calculate dynamic stopping distances calibrated to velocity and payload weight. Safety zones adapt automatically during turning arcs, preventing false-positive trips while ensuring 100% personnel protection.
VDA 5050 Standard Interface Protocol
Eliminate vendor lock-in. Our factory fleets support the universal VDA 5050 communication interface, enabling seamless fleet-level interoperability across diverse third-party AGV brands, legacy conveyor PLCs, rapid high-speed roll doors, and enterprise ERP/WMS platforms (SAP, Oracle, Manhattan Associates).
Mission-Critical Application Scenarios for Magnetic Guidance
Deploying specialized autonomous vehicles across challenging production lines, cold-storage distribution, and sensitive electronic manufacturing.
Automotive Assembly & Powertrain Lines
Continuous synchronized movement through body-in-white (BIW) and engine dressing lines demands millisecond tracking reliability. Magnetic tape lines embedded flush beneath protective polyurethane coatings guarantee zero sensor drift despite metallic framing, welding spatter, and high magnetic coil interference nearby.
Sub-Zero Cold Chain & Freezer Warehousing
In -25°C cold-storage logistics, optical lenses frequently suffer condensation fogging and frost buildup during zone transfers. Magnetic tape navigation operates via pure magnetic flux, requiring zero optical transparency, delivering uncompromised 24/7 pallet transfer without expensive defrost cycle downtime.
Semiconductor Cleanrooms & Chemical Plants
Class 100 cleanroom environments forbid floor flaking and particulate emissions. Synthetic magnetic adhesive tracks or slotted embedded magnetic rods produce zero airborne particulate debris, meeting strict ISO 14644-1 cleanroom certifications while ensuring spark-free, explosive-proof (ATEX) material transport.
Total Cost of Ownership (TCO) & Lifecycle Economics
A rigorous five-year financial projection evaluating capital investment, site infrastructure maintenance, and direct labor replacement economics.
Rapid Payback Period (<14–18 Months)
By replacing three shifts of certified forklift operators across 24/7 operating cycles, an automated magnetic forklift pays for itself rapidly. Considering direct driver wages, payroll taxes, insurance overhead, and fork-truck lease rates, a dual-vehicle automated cell regularly delivers net-positive cash flow within year two.
Near-Zero Facility Downtime During Install
Deploying magnetic guide tracks requires no ceiling reflectors, elevated surveyed targets, or complete warehouse map resets. Typical factory loops can be laid out over a single weekend with industrial adhesive tape, achieving full live commissioning without interrupting factory shift throughput.
99% Reduction in Inventory & Asset Damage
Human operator errors constitute over 85% of warehouse rack strikes, pallet drop damage, and door collision costs. Laser and magnetic sensor arrays enforce strict velocity profiles, controlled deceleration curves, and soft-docking fork insertion, virtually eliminating pallet payload loss.
Frequently Asked Questions: Technical & Sourcing Authority
Authoritative technical guidance compiled by robotics engineers to streamline supplier evaluation and system specification.
Under standard warehouse conditions, top-grade industrial synthetic rubber magnetic tape with acrylic structural adhesive withstands moderate pneumatic and polyurethane wheel crossover. However, in heavy traffic zones with 3-ton manual counterbalanced forklifts, the industry standard practice is to cut a shallow 2 mm to 3 mm floor slit, press the magnetic strip flush with the surface, and encapsulate it with high-strength industrial epoxy or polyurethane grout. This method renders the track practically indestructible with a operational lifespan exceeding 8 to 10 years.
Yes. This architecture is defined as "Dual Hybrid Navigation." In open staging bays and flexible loading zones, the vehicle uses Laser SLAM to calculate dynamic obstacle bypass paths and long-distance transit. When interfacing with narrow high-bay racking systems, robotic machine loading cells, or automated palletizers requiring sub-millimeter precision, the vehicle seamlessly locks onto magnetic floor strips for deterministic terminal guidance.
Branching, turning, and precise station positioning are triggered using magnetic polarity markers (alternating North-South polarities) or passive RFID floor tags embedded beside the guide strip. When the AGV's auxiliary magnetic sensors or RFID reader detects a polarity shift (e.g., dual South poles), the onboard controller executes branch selection, speed deceleration, or station stopping procedures dictated by the dispatch system.
Our systems deploy industrial Wi-Fi (802.11 a/b/g/n/ac 5.8 GHz roaming) or private 5G industrial networks. Communication interfaces support VDA 5050 protocols, RESTful JSON APIs, WebSocket streams, and standard Modbus TCP/IP. This ensures bidirectional data handshakes with MES, WMS, and ERP systems (SAP, Oracle, Kingdee) for live task allocation, battery state telemetry, and dynamic rack queue status.
Overseas enterprise buyers should demand CE Machinery Directive certification under EN ISO 3691-4:2023, EMC Directive 2014/30/EU compliance, and Low Voltage Directive 2014/35/EU. For North American deployment, UL 3100 (Outline of Investigation for Automated Mobile Platforms) and ANSI/ITSDF B56.5 are essential. Our factory delivers full third-party test reports and Declarations of Conformity with all exported models.
We maintain centralized spare parts depots with guaranteed 48-hour air-dispatch for critical electronics (sensors, controllers, drive motors). Furthermore, through remote VPN diagnostic tunnels into the fleet management server, our Tier-3 field engineers provide 24/7 technical dispatch and software updates, minimizing overseas site downtime.
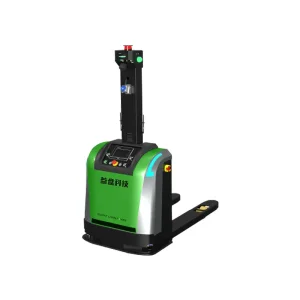
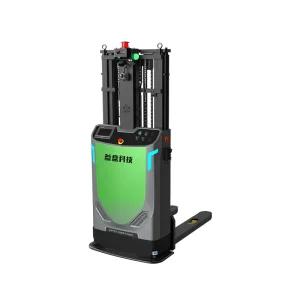
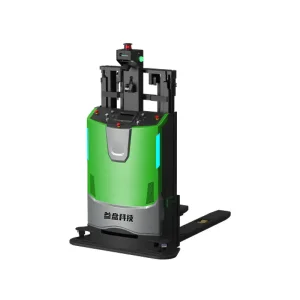
High-Capacity Automated Pallet Handling & Stacker Solutions
Complete your facility's internal transport automation with high-lift stackers, heavy-capacity counterbalanced automated forklifts, and versatile robotic chassis.

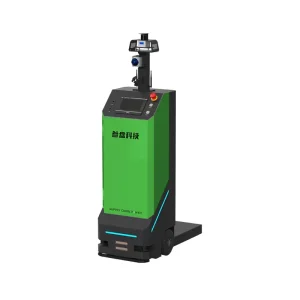
Standard Project Parameters for Rapid RFQ & Solution Engineering
Prepare your facility parameters to receive a formal simulation layout, equipment bill of materials, and guaranteed factory quotation within 24 hours.
1. Pallet Topology & Payload
Specify standard pallet dimensions (Euro 1200x800, Industrial 1200x1000, US 48x40), bottom board design (perimeter base vs. open-bottom), payload center of gravity, and maximum static/dynamic weights (from 300 kg to 3,000 kg).
2. Spatial Dimensions & Heights
Detail clear aisle widths between racking stanchions, minimum turning radiuses at intersection junctions, top beam stacking heights (up to 4,500 mm), and overhead clearance limitations including roll doors and ductwork.
3. Cycle Throughput & Systems
Determine hourly pallet transfer rates, number of operational shifts (single, double, or continuous 24/7), floor material (polished concrete, epoxy, tiled), and target ERP/WMS interface requirements (VDA 5050, Modbus, API).