High-Precision AGC & Laser SLAM Mobile Fleets
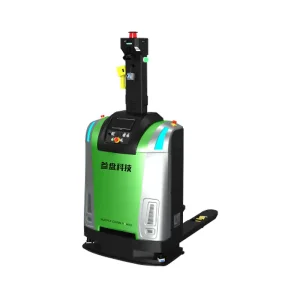
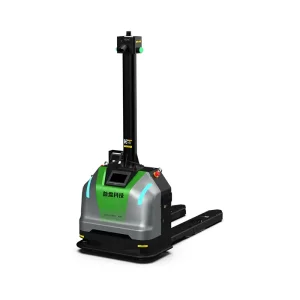
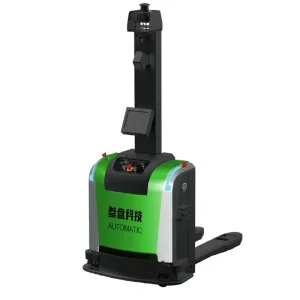
Explore China's next-generation automated guided carts (AGC) and laser-guided autonomous forklifts engineered for rapid, reflector-free warehouse commissioning.

Executive Summary: The Geopolitical & Technological Evolution of China AGC Factories
In the contemporary landscape of global intralogistics and digital manufacturing, the search query "China AGC Automation Factory & Factories" represents far more than a transactional procurement inquiry. It denotes an enterprise-level transition toward automated material transport, where automated guided carts (AGC), automated guided vehicles (AGV), and autonomous mobile robots (AMR) replace capital-intensive, accident-prone manual workflows. Over the last decade, China has transformed from an assembly hub for legacy magnetic-stripe guided carts into the world's most dense cluster of advanced robotics manufacturing centers, delivering native Laser SLAM (Simultaneous Localization and Mapping), hybrid navigation architectures, and multi-tier fleet intelligence.
Industrial decision-makers from North America, Europe, Southeast Asia, and the Middle East are re-evaluating their capital equipment supply chains. Historically, European and Japanese automation vendors commanded premium pricing with lead times exceeding 9 to 14 months. Conversely, Chinese automated guided cart manufacturers—bolstered by mature supply chain integration, domestic core-component fabrication (LiDAR, drive-steering units, safety PLCs, and high-discharge lithium iron phosphate batteries), and vast domestic testbeds in consumer electronics and electric vehicle (EV) gigafactories—now deliver equal or superior kinematic performance at a fraction of total cost of ownership (TCO). This technical white paper examines the engineering differentiators, systemic factory advantages, deployment workflows, and procurement verification frameworks that govern industrial AGC automation in China.
Why Tier-1 Chinese AGC Automation Factories Lead the Intralogistics Sector
A granular look at the four architectural pillars enabling Chinese robotic manufacturing hubs to outpace international competitors in delivery velocity and performance density.
Full Supply Chain Vertical Integration
Unlike Western systems integrators who outsource chassis welding, sensor fusion, and motion control to separate vendors, Chinese AGC plants operate within unified industrial clusters (such as Jiangsu-Zhejiang, the Pearl River Delta, and Chengdu's advanced equipment corridor). Drive motors, optical encoders, precision reducers, LiDAR sensors, and battery management systems (BMS) are sourced within a 50-kilometer radius, drastically reducing Bill of Materials (BOM) overhead and compressing engineering lead times to under 30 days.
Native Laser SLAM & Reflector-Free Agility
Traditional AGCs were constrained to magnetic strips glued to warehouse concrete or high-contrast QR matrix codes that tore under forklift traffic. Modern Chinese factories have standardized on 2D/3D Laser SLAM. By reading natural structural landmarks (columns, walls, static shelving), these robots map facilities up to 400,000 m² without modifying physical civil infrastructure. Facilities can pivot operational layouts via digital map updates in hours rather than incurring weeks of floor renovations.
Open Firmware & RESTful API Ecosystem
Vendor lock-in represents one of the largest hidden risks in enterprise automation. Proprietary protocols from legacy providers often force end-users to contract exclusive service teams for minor route modifications. Leading Chinese AGC factories design around open API ecosystems: robot controllers (such as the proprietary SCC architecture) interface directly via JSON-RESTful APIs, MQTT, OPC-UA, and Modbus TCP with standard MES (Manufacturing Execution Systems), WMS, and ERP platforms (SAP, Oracle, Blue Yonder).
Industrial Stress-Testing & Real-World Validation
China's internal market serves as the most demanding proving ground worldwide. High-velocity e-commerce logistics parks handle hundreds of thousands of parcels each night, while automotive manufacturing plants operate continuous 24/7 lines. Chinese AGC models undergo continuous multi-thousand-hour validation runs in high humidity, sub-zero cold storage (-25°C), and dusty manufacturing environments before achieving export designation, guaranteeing high Mean Time Between Failures (MTBF > 20,000 hours).
Kinematic & Navigational Paradigm Comparison
Procurement teams must distinguish between obsolete magnetic-guided carts and modern natural-contour Laser SLAM AGC/AMR systems. The following table contrasts legacy baseline standards with modern factory specifications manufactured across China's leading production lines:
| Evaluation Parameter | Legacy AGC (Magnetic Tape / Optical Stripe) | Reflector-Based AGV (Laser Targets) | Modern Chinese Laser SLAM AGC / AMR |
|---|---|---|---|
| Civil Infrastructure Modification | Extensive; magnetic tape slicing, epoxy recoating, recurring track repairs | Moderate; survey-grade laser reflectors affixed to every column/wall | Zero civil modification; natural contour feature mapping |
| Docking & Positioning Precision | ±15 mm to ±25 mm depending on magnetic wear | ±10 mm under clean optical line-of-sight | ±5 mm (optical/LiDAR dual-sensor fusion) |
| Deployment & Commissioning Cycle | 4 to 8 weeks per warehouse zone | 3 to 6 weeks (reflector alignment and surveying) | 1 to 3 days (1-Day rapid mapping on compatible floors) |
| Dynamic Obstacle Avoidance | Emergency bumper stop only; zero detour routing | Fixed stopping zone; cannot navigate around dropped pallets | Autonomous real-time rerouting via 3D ToF obstacle cameras |
| Fleet Scalability | Rigid linear routes; collisions common at intersections | Complex central PLC dispatch; high software cost | Distributed algorithmic dispatch (Server X Store / 200+ units) |
| Route Reconfiguration Cost | High; physical tape stripping and floor re-grooving | High; reflector relocation and optical re-surveying | Zero physical cost; CAD map redraw via cloud terminal |
This fundamental shift from hardware-bound navigation to software-defined spatial intelligence allows international end-users to achieve true flexibility. If an automotive assembly plant transitions from one chassis variant to another, operators do not call civil contractors to alter ground tracks; they load a new operational topology through the web-based fleet console in minutes.
Localized Industry Scenarios & Real-World Operating Workflows
Examining field-deployed automation architectures across high-stakes manufacturing and distribution environments.
Automotive & EV Battery Gigafactories
In high-rate automotive assembly lines, uncrewed AGCs navigate narrow line-side corridors (under 1.2 m clearance) to supply battery modules, chassis sub-assemblies, and heavy stamping dies directly to robotic workstations. Integrated low-profile top-lifting chassis (such as the AMB-CSW10-BH series) slide underneath customized rack trollies, lift 1,000 kg loads with millimeter precision, and synchronize with the line's cycle time (Takt time) to eliminate manual replenishment delays.
High-Throughput FMCG & Retail Distribution
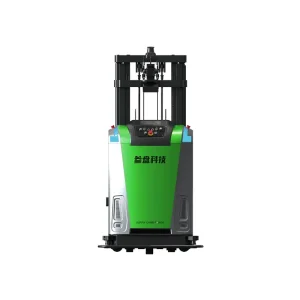
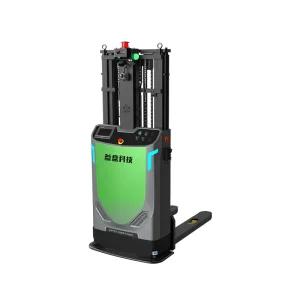
Fast-Moving Consumer Goods hubs require rapid cross-docking, buffering, and high-bay stacking. Utilizing automated counterbalanced and stacker forklifts (SFL-CDD15 / SFL-CPD20-Y), the system performs multi-tier pallet storage up to 3 meters without human operators. 3D visual perception dynamically identifies pallet pocket pitch and orientation, adjusting fork tines in real time to prevent rack collisions or dropped goods.
Cold Chain & Deep-Freeze Food Processing
Human operators face extreme safety hazards and reduced productivity in blast-freeze warehouses operating at -20°C to -30°C. Specialized cold-chain AGC systems feature heated sensor housings, low-temperature anti-condensation LiDAR optical windows, and cold-stabilized lithium iron phosphate battery chemistries. Fleets autonomously transition from ambient dock areas to sub-zero freezer vaults while eliminating condensation build-up through controlled thermal transition zones.
Pharmaceutical & 3C Electronics Cleanrooms
Semiconductor wafer fabrication and sterile pharmaceutical packaging demand ISO Class 4 / Class 5 cleanroom conditions where human particulate shedding must be minimized. Cleanroom-certified Chinese AGCs utilize polyurethane non-marking antistatic drive wheels, sealed brushless motors, enclosed mechanical lifting actuators, and localized HEPA filtration exhausts to ensure particulate emissions remain well below strict international threshold limits.
Turnkey Intralogistics Architecture: From Silicon to Enterprise Software
A single AGC is simply an unguided motor without an overarching computational architecture. Tier-1 automation factories deliver an integrated three-tier stack: the hardware motion layer, the local real-time controller layer, and the overarching fleet dispatch / Supply Chain Control Tower.
Three-Tier Industrial Automation Architecture
Full-stack alignment between on-chassis edge computing, local routing engines, and corporate ERP systems.
Tier 1: Onboard SCC Controller
- Dual ARM Cortex-A72 + FPGA real-time kernel
- Real-time Laser SLAM point-cloud processing (20 Hz)
- Hardware-level SIL-2 / PLd safety interlock circuits
- Dual CANopen / EtherCAT high-speed motor bus
- Autonomous battery state estimation (SOC/SOH)
Tier 2: Server X Store Fleet Dispatch
- Dynamic time-space path planning (Voronoi algorithms)
- Simultaneous multi-vehicle deadlock avoidance
- Traffic density balancing across aisle choke points
- Automatic opportunity-based fast charging dispatch
- High-availability hot-standby clustering
Tier 3: Control Tower & Integration
- Bi-directional WMS / MES / ERP integration (JSON/REST)
- Real-time digital twin visualization of all warehouse nodes
- Predictive maintenance alerts via vibration & thermal logging
- Comprehensive audit trails compliant with FDA / GMP
- Global multi-site centralized telemetry monitoring
Global Enterprise Procurement Framework: Evaluating China AGC Factories
A rigorous audit guide for engineering directors, procurement managers, and systems integrators preparing an international RFP.
1. International Safety Compliance Verification
Overseas procurement teams must require full third-party test reports validating ISO 3691-4:2023 (Driverless industrial trucks and their systems) and EN ISO 13849-1 (PLd Cat 3). Never accept self-declarations. Ensure that safety field LiDARs, e-stop interlocks, and speed monitoring functions execute over certified safety-rated hardware buses.
2. Factory Continuous Burn-In Protocols
Audit the factory's pre-shipment Quality Assurance regime. Leading Chinese AGC facilities operate dedicated indoor test tracks where every manufactured vehicle undergoes a continuous 72-to-120 hour loaded burn-in cycle. Test documentation should log battery thermal curves, drive-gear oil temperatures, encoder drift, and LiDAR point cloud consistency under simulated vibration.
3. Cybersecurity & Software Autonomy
Industrial IoT infrastructure must comply with corporate IT firewalls (IEC 62443 cybersecurity standard). Confirm that fleet management servers can be deployed fully on-premises in air-gapped server environments without requiring unvetted outbound internet connections or non-transparent remote telemetry tunnels.
4. International Spares & Modular Field Service
Prioritize manufacturers that utilize standardized modular sub-assemblies. Drive wheel units, lift cylinders, safety sensors, and logic modules should be field-swappable in under 30 minutes. Verify that the supplier maintains regional spare-parts hubs or provides comprehensive emergency spare kits alongside factory training for in-house plant maintenance technicians.
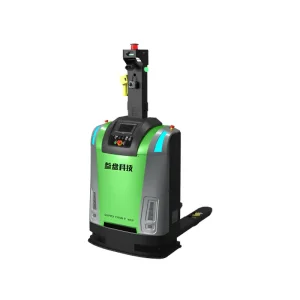
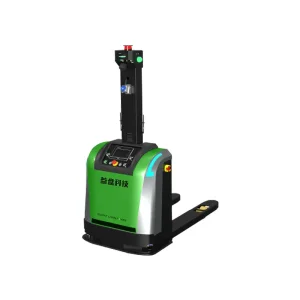
Advanced Stacking, Narrow-Aisle & Modular AGC Fleets
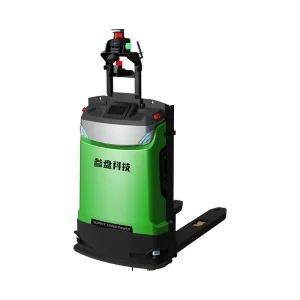
Explore heavy-load and high-reach laser SLAM autonomous forklift series manufactured for vertical warehousing, rack stacking, and multi-tier production flows.
Frequently Asked Questions: Sourcing AGC Automation from China
In-depth engineering and commercial answers to the most common queries submitted by global plant engineers and logistics directors.
Historically, an AGC (Automated Guided Cart) referred to a compact, low-profile towing or under-riding cart governed by simple magnetic tape, carrying payloads up to 1,000 kg. An AGV (Automated Guided Vehicle) traditionally represented larger, specialized mobile industrial equipment (such as counterbalanced forklifts or heavy-duty reach trucks). An AMR (Autonomous Mobile Robot) signifies unconstrained natural-navigation vehicles using LiDAR and SLAM. Today, modern Chinese automation factories have converged these categories: state-of-the-art AGCs feature full Laser SLAM autonomy without magnetic strips, effectively functioning as industrial-grade AMRs with the robust mechanical payload capacities of traditional AGVs.
Laser SLAM uses multi-sensor fusion. The onboard SCC controller continuously cross-references high-frequency 2D/3D LiDAR point clouds against an internally constructed topological grid map. Odometry data from wheel optical encoders and solid-state inertial measurement units (IMUs) compensates for high-speed wheel slip. For final physical pallet engagement, high-resolution 3D Time-of-Flight (ToF) cameras and laser line profilometers scan the pallet pocket apertures or docking pin receptors, calculating real-time 6-DoF offset adjustments that drive the steering servo motors to within ±5 mm of target alignment.
Most international projects achieve comprehensive CapEx payback within 12 to 18 months. In high-wage jurisdictions (North America, Western Europe, Australia), where fully loaded round-the-clock forklift driver labor costs range from $65,000 to $90,000 per operator per shift, a three-shift facility saves roughly $200,000 annually per converted workstation. Coupled with a 99% reduction in structural racking and cargo impact damage, plus zero civil floor reconstruction costs, the total cost of ownership (TCO) advantage of Chinese AGC fleets is mathematically indisputable.
Tier-1 export manufacturers partner with internationally recognized notified testing bodies (such as TÜV Rheinland, TÜV SÜD, SGS, and Intertek) to conduct type-examination certifications. Verification adheres strictly to ISO 3691-4:2023 for driverless trucks, EN 1175:2020 for electrical systems, and UL 583 / ANSI/ITSDF B56.5 for North American markets. Overseas buyers receive comprehensive technical construction files (TCF), safety circuit schematics, and functional safety verification certificates covering PLd/SIL-2 emergency stops and speed-dependent laser monitoring fields.
Factory software architectures do not enforce proprietary locks. Fleets integrate through standard industry middleware using RESTful JSON APIs, WebSockets, MQTT brokers, or industrial fieldbuses (OPC-UA, Modbus TCP, PROFINET). The fleet controller connects to tier-1 enterprise WMS/MES platforms (SAP EWM, Manhattan Associates, Blue Yonder, Oracle NetSuite) via clean, documented endpoints, allowing standard inbound transport orders, pick calls, and pallet drop confirmations to exchange in under 50 milliseconds.
Vehicles are equipped with industrial-grade Lithium Iron Phosphate (LiFePO4) or high-density NMC cells featuring intelligent BMS with CAN communication. Systems support two continuous operation paradigms: High-Rate Opportunity Charging (in which vehicles automatically dock with floor charging shoes at up to 1C rates during 15-minute idle breaks, achieving 24/7 perpetual operation) and Manual/Automated Battery Swap, where hot-swappable battery packs are exchanged in under 2 minutes to maintain continuous line-side availability.
Modern deployments utilize a hybrid service model. First-time map recording and path simulation can be completed in as little as 1 day. In situations without on-site factory technicians, engineering teams utilize encrypted remote virtual private tunnels to configure nodes, tune motion PIDs, and conduct live acceptance runs. Replacement wear items (vulcanized polyurethane drive treads, optical proximity sensors, relays, contactor blocks) are cataloged under open international OEM part numbers, enabling local procurement directly from industrial distributors worldwide.
To receive a turnkey simulation model and precise price quote, buyers should provide: (1) Standard pallet specifications (dimensions, bottom board configuration, bottom runner clearance, maximum gross weight); (2) High-resolution architectural drawings (CAD .dwg or dimensioned PDF) indicating main traffic lanes, transfer buffer stations, and structural building columns; (3) Daily movement volume targets per hour across each operational shift; and (4) Floor surface specifications (concrete flatness under DIN 18202 or ASTM E1155, presence of floor expansion joints, and surface coatings).
Begin Your Engineering Audit & System Simulation
Connect directly with our automation systems engineers in Chengdu, China. Send your warehouse CAD layout and throughput targets for a customized fleet kinematic analysis, cycle time calculation, and turnkey factory proposal.