High-Accuracy Transport & Dynamic In-Line Sorting Systems
Engineered for high-throughput export warehouses, packaging plants, and distribution centers operating in San José, Alajuela, and Limón.

Dynamic Weighing & Sorting Automation: The Costa Rican Paradigm
Bridging traditional agricultural excellence with modern MedTech manufacturing through high-speed weight verification and automated sorting ecosystems.
1. Industrial Backdrop: Why Costa Rica Demands Precision In-Line Dynamic Sorting
Costa Rica’s economic landscape occupies a unique intersection in Central America. On one hand, it remains an indispensable global exporter of perishable produce—commanding major international supply chains in pineapples, Cavendish bananas, specialty Arabica coffees, and exotic fruits. On the other hand, the nation has evolved into Latin America's premier hub for Life Sciences, Medical Devices (Class I, II, and III), and advanced electronics assembly, anchored within duty-exempt Zona Franca (Free Trade Zone) clusters like Coyol and Global Park.
Both sectors encounter a universal challenge: regulatory compliance and margin volatility. In agro-exporting, international supermarket chains enforce strict tare weight declarations, net-weight accuracy, and size grading. Even a 2% product give-away per carton erodes hundreds of thousands of dollars annually, while underweight shipments face severe rejection penalties at North American and European ports. Simultaneously, medical device manufacturers require 100% weight-based completeness verification to detect missing instruction leaflets, seals, or micro-components inside sealed sterile barrier pouches.
Chinese-manufactured dynamic sorting scales bridge this critical void. By combining precision high-speed strain gauge or electromagnetic force restoration (EMFR) load cells with rugged IP65/IP69K stainless steel designs, our sorting equipment ensures exact classification, real-time rejection of non-compliant units, and non-stop continuous operation under both tropical humidity and hygienic cleanroom protocols.
2. Global Sourcing Trends: The Shift Toward Turnkey, Modular Weighing Systems
Historically, Central American enterprises relied on European or North American integrators for checkweighing and sorting machinery. However, long procurement lead times (often 32–40 weeks), prohibitive capital expenditures (CapEx), and exorbitant proprietary replacement parts have pushed supply chain directors to reassess their global sourcing strategies.
China's smart manufacturing infrastructure has restructured this paradigm. Modern Chinese manufacturers offer dynamic sorting scales, multi-head sorting apparatus, and automated pallet scales engineered around open protocols (Modbus-TCP, Profinet, Ethernet/IP, and RESTful APIs). This ensures frictionless integration with existing warehouse management systems (WMS) and manufacturing execution systems (MES), while reducing equipment acquisition expenditure by 40% to 60% compared to legacy Western alternatives.
Engineering Superiority: China Factory Efficiency Advantages
Why leading multinational enterprises and local Costa Rican packhouses partner with tier-1 Chinese sorting scale manufacturers.
Advanced Metrology & DSP Algorithms
Our sorting scale terminals utilize proprietary High-Speed Digital Signal Processing (DSP) and intelligent dynamic vibration filtration. This nullifies ambient floor vibration from forklifts and conveyor lines, guaranteeing consistent milligram-level readings at speeds exceeding 120–180 cycles per minute.
Robust Mechanical Craftsmanship
Fabricated using food-grade SUS304 and medical-grade SUS316L stainless steel, every scale bed features laser-cut seams, tool-free belt removal for rapid sanitization, and IP67 washdown ingress protection built to resist corrosive sanitizing chemicals and equatorial ambient humidity.
Integrated Autonomous Logistics
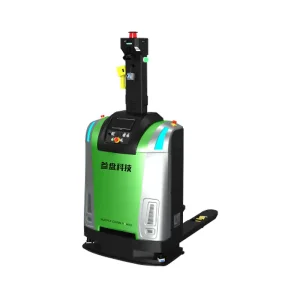
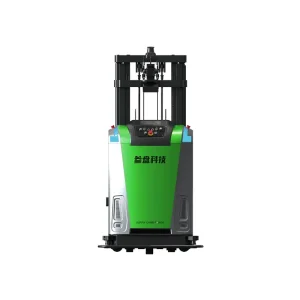
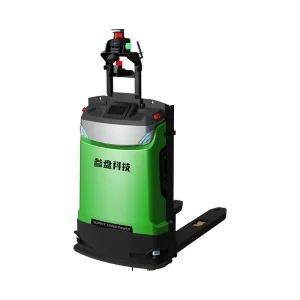
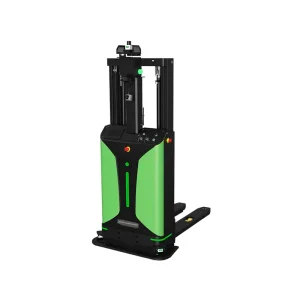
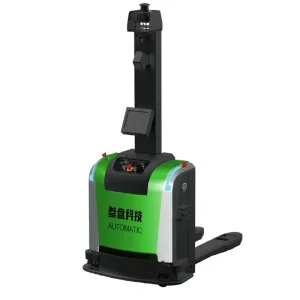
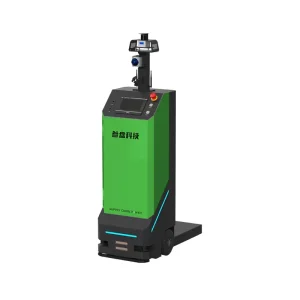
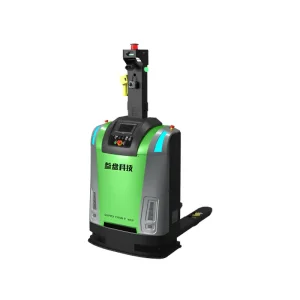
Unlike standalone scale vendors, our Chinese manufacturing ecosystem unites in-line weight inspection directly with Laser SLAM autonomous forklifts, top-lifting AMRs, and automatic multi-gate sorters, providing end-to-end material flow from carton packaging to container staging.
Tailored Deployment Across Costa Rica’s Strategic Sectors
Purpose-built installations solving high-speed grading, checkweighing, and automated handling challenges.
Export Agricultural Packaging Plants
In Limón, Sarapiquí, and San Carlos, our high-capacity sorting scales accurately weigh and grade boxes of bananas, pineapples, and tubers. Multi-level flipper or air-blast rejects segregate produce into exact weight classes to maximize carton fill efficiency while generating instant lot-level yield analytics.
Life Sciences & MedTech Cleanrooms
Deployed within Coyol Free Zone medical device production cells, ultra-sensitive checkweighing scales verify surgical kit assembly lines. Detecting deviations as fine as 0.02 grams prevents incomplete catheter or implant packages from progressing to final sterilization.
FMCG & Retail Fulfillment Hubs
Across central distribution centers near San José, floor sorting scales (like the SCP101/SCP100) integrated with AMRs manage carton scanning, tare verification, and direct route assignment for quick replenishment of regional retail store networks without human data entry errors.
Global Enterprise Requirements & Future Engineering Trends
A comprehensive assessment guide for industrial procurement directors, warehouse architects, and operations managers.
Key Technical Criteria Demanded by International Procurement Teams
When sourcing dynamic sorting scales and complementary automated material handling equipment from China, enterprise procurement teams prioritize measurable KPIs over marketing rhetoric:
- OIML / NTEP Certifications: Compliance with OIML R51 Class XIII/XIV recommendations for automatic gravimetric checkweighers ensures legal-for-trade certification across Latin American export ports.
- Interoperability & Fieldbus Protocols: Direct connection via industrial fieldbus cards (PROFINET, EtherNet/IP, Modbus TCP) to bypass siloed machine architectures and connect real-time weight trends directly into SCADA and plant ERP systems.
- Mean Time Between Failures (MTBF) & Spare Parts Availability: Sourcing machines that employ standard, non-proprietary wear parts (Schneider electrical components, Omron sensor suites, and standard food-grade conveyor belting) enables maintenance teams to maintain local redundancy.
- Total Cost of Ownership (TCO): Factoring in initial equipment cost, freight to Puerto Limón or Puerto Caldera, commissioning duration, electrical consumption, and remote diagnostic capabilities.
Future Trends: Convergence of Sorting Scales with Laser SLAM Robotics
The global material handling industry is moving rapidly toward continuous automated loops. Standalone sorting scales are no longer isolated islands. In cutting-edge facilities, dynamic weighing data directly informs fleet management algorithms. If an outbound pallet or carton deviates from the expected weight curve, autonomous Laser SLAM forklifts automatically redirect the unit to quality quarantine bays without human manual intervention, reducing operational friction and ensuring total zero-defect logistics.
Frequently Asked Questions (FAQ)
Critical answers for engineers and purchasing managers procuring Chinese industrial sorting scales for Costa Rica.
How do Chinese dynamic sorting scales maintain accuracy in Costa Rica’s humid coastal climates?
Can our engineering team connect the sorting scales directly to SAP, Oracle, or local WMS?
What rejector mechanisms are available for different package weights and shapes?
What is the typical shipping transit time and support structure from China to Costa Rica?
How do floor sorting scale systems coordinate with autonomous forklifts and AMRs?
Complete Autonomous Material Handling Fleet for Costa Rica
High-load pallet trucks, stacking forklifts, and AGV platforms ready for seamless factory and warehouse automation upgrades.